Call Us For Your Battery Needs
800-400-4858
Who Are the Best Aluminum Profile Manufacturers in China?
China’s aluminum industry operates at an exceptional scale, but scale alone does not identify the right supplier. The US Geological Survey’s Mineral Commodity Summaries 2025 estimates that China produced 43 million tonnes of primary aluminum in 2024, out of roughly 72 million tonnes worldwide. This figure describes metal production, not finished profiles. Still, it helps explain why China has a deep manufacturing base for extrusion, surface treatment, and custom fabrication.
The best Aluminum Profile manufacturers depend on what a project actually needs. A window-system buyer may prioritize consistent 6063 alloy, tight dimensional tolerances, and durable anodizing. A solar-frame buyer may care more about repeatable lengths, drilled features, and dependable delivery. Look closely at sample parts, inspection records, production equipment, and how clearly a factory explains its process. Ask for evidence, not just a polished catalog. The scale is enormous.
This guide compares Chinese manufacturers through practical criteria: product range, engineering support, quality controls, customization, and export experience. A supplier’s certifications can be useful, but they do not prove that every batch will meet your requirements. Nor is there one universal “best” company; rankings shift with alloy, finish, order volume, and destination. That makes selection less tidy than a list suggests. Buyers should confirm specifications, inspect samples, and discuss testing before placing large orders. A careful comparison cannot remove every risk, but it can make the choice more informed.
How Aluminum Profile Manufacturing Works in China
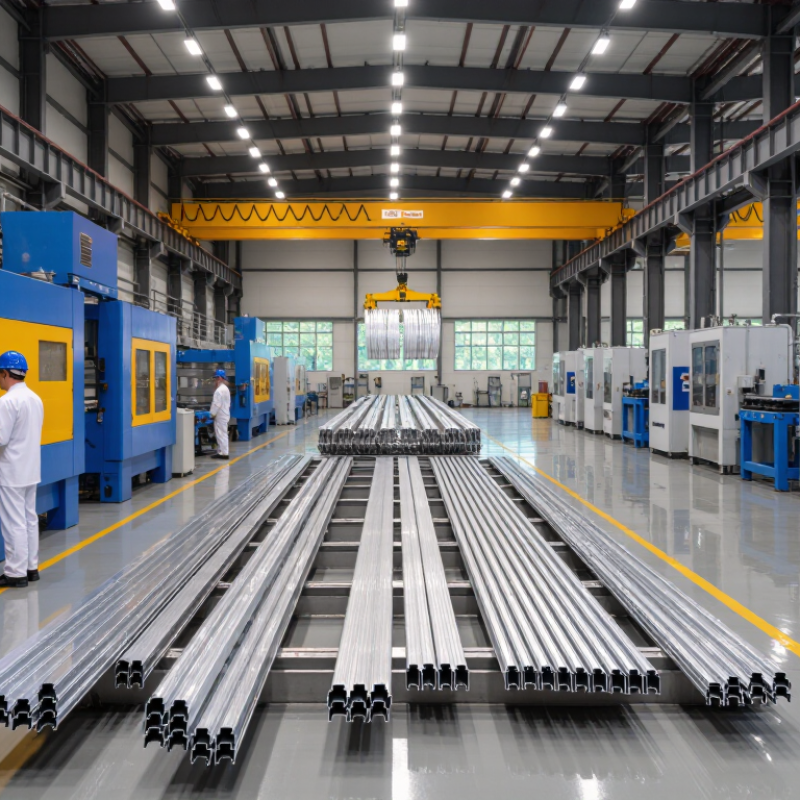
Aluminum profile manufacturing in China often begins with alloy selection and billet preparation. The billet is heated, then pushed through a shaped steel die to create a continuous profile. A tiny change in die design can affect wall thickness, corner sharpness, and how easily parts fit together. After extrusion, profiles are cooled, stretched to reduce distortion, and cut to length. Small details matter.
Heat treatment can improve strength, while surface finishing may include anodizing or powder coating. Not every finish suits every use. For example, an outdoor frame needs different corrosion protection from an indoor display rail. Manufacturers typically inspect dimensions, surface appearance, and mechanical properties, but inspection methods and sampling rates vary. Buyers should confirm what checks are included rather than assume every factory follows the same routine. Even a well-run line can produce occasional variation; that possibility deserves honest discussion.
Tips: Share drawings, alloy requirements, finish, and acceptable tolerances before production. Ask for a sample and a written inspection plan. Check packaging details too, since long profiles can be scratched or bent in transit. A clear specification prevents avoidable rework.
Who Are the Best Aluminum Profile Manufacturers in China? - How Aluminum Profile Manufacturing Works in China
Use this process-and-evidence guide to understand aluminum profile production and assess suppliers. Capabilities and specifications vary by factory, alloy, profile design, and order requirements.
| Production stage | How it works | Key equipment or capability | Useful checks and supplier evidence |
|---|---|---|---|
| 1. Alloy and billet selection | Aluminum billets are selected to suit the required strength, corrosion resistance, formability, and finishing needs. Common extrusion alloys include 6063 and 6061, but the appropriate choice depends on the application. | Controlled material sourcing, billet handling, and traceability systems. | Request the proposed alloy and temper, material documentation, and a method for tracing production batches. |
| 2. Die design and preparation | A heated billet is pushed through a shaped die to create a continuous profile. Die design affects wall thickness, dimensional consistency, surface quality, and how easily a shape can be extruded. | Die design and machining capability, die maintenance, and experience with the requested profile geometry. | Review the profile drawing, critical dimensions, proposed tolerances, and whether a production sample or first-article approval is available. |
| 3. Extrusion | The press forces the billet through the die. Extruded material exits as a continuous shape and is handled on a run-out system before being cut to manageable lengths. | Press capacity suited to the profile's dimensions, weight, and complexity, along with appropriate handling equipment. | Ask how the supplier confirms press suitability and controls profile dimensions and visible surface defects during production. |
| 4. Cooling and quenching | After leaving the die, the profile is cooled. The cooling method and conditions depend on the alloy, profile, and required properties. | Controlled cooling equipment and handling that limits distortion and damage. | Confirm that the cooling process is defined for the specified alloy and temper and that any required mechanical properties are verified. |
| 5. Stretching and straightening | Profiles may be stretched to reduce residual stresses and improve straightness before being cut to length. The exact process depends on the product and specification. | Stretching equipment, straightness measurement, and careful length cutting. | Agree on straightness, length, and dimensional requirements in the drawing or purchase specification. |
| 6. Heat treatment and aging | When required for the specified alloy and temper, controlled heat treatment develops the intended mechanical properties. Not every profile uses the same treatment. | Temperature-controlled furnaces, production records, and procedures appropriate to the alloy and temper. | Specify the required temper and property criteria; ask for relevant test records when these properties are part of the order requirements. |
| 7. Machining and fabrication | Profiles may be cut, drilled, milled, punched, or assembled after extrusion to meet the finished-part drawing. | Appropriate cutting and machining equipment, workholding, and process control for the part's tolerances. | Check sample parts against the drawing, including hole locations, cut lengths, fit, and any specified burr or edge requirements. |
| 8. Surface finishing | Depending on the application, profiles can be supplied unfinished or given treatments such as anodizing or powder coating. Finish requirements should be defined for the intended environment and appearance. | In-house or qualified finishing capacity, process control, and protection of finished surfaces during handling. | Specify finish type, color, appearance, and applicable performance tests. Request inspection records for the requirements that matter to the application. |
| 9. Inspection and shipment | Finished profiles are inspected, identified, packed, and prepared for transport. Inspection scope should match the agreed drawings and order specifications. | Measurement tools, inspection procedures, batch identification, and packaging appropriate to profile length and finish. | Review sample inspection reports, traceability, packaging details, and any quality-management certificates required by the buyer. |
| 10. Supplier evaluation | A suitable manufacturer is one whose demonstrated process, quality controls, technical support, and delivery capability match the product requirements—not simply the one with the lowest quotation. | Relevant extrusion and finishing capacity, engineering support, stable quality systems, and a clear process for handling nonconforming product. | Compare approved samples, written specifications, quality records, capacity and lead-time commitments, communication, and corrective-action practices. |